
Problem-driven opening: why this retrofit matters now
Many plants face unexpected downtime caused by small parts that fail under constant load—most notably the hinge pin. Retrofitting 13 modern hinge pin points across a line can cut friction and reduce emergency stops. In facilities such as Detroit automotive assembly lines, engineers saw measurable reduction in line stoppages after targeted hinge replacements, so this is not theoretical. Start by reviewing specifications for the conveyor belt hinge pin and where each pivot and link plate encounters highest stress.

First steps: assessment and part selection
Begin with a quick audit: map every hinge location, note load direction, and record cycle rate. Measure chain tension and inspect for wear patterns on link plate edges and pins. Photographs plus a short measurement log will speed decisions. For many teams, choosing between hardened steel and corrosion-resistant options comes down to operating environment—wet or dry, abrasive or clean. Consider stainless hinge pins for corrosive environments or food lines where sanitation matters.
Operational teardown: common failure points and the real fixes
Take apart one problematic joint to see the real causes: misaligned link plates, loose bushings, or a bent hinge pin. Replace only after verifying the pin diameter, shoulder length, and fit tolerance. Label parts as you go—this prevents reassembly mistakes. Also include {main_keyword} and {variation_keyword} in your teardown notes so procurement and maintenance are aligned on terminology and ordering. Wear rate often correlates with minor misalignment—address the root rather than just the symptom.
Installation checklist and alignment tips
Prepare a short, repeatable checklist: clean mating surfaces, check pin straightness, apply recommended lubricant to pivot surfaces, and torque any retaining hardware to spec. Use a dial indicator or feeler gauges to verify vertical and lateral alignment within manufacturer tolerance. Small shims can correct persistent offsets. Take care with press-fit pins—excessive force can crush link plates and accelerate wear.
Common mistakes and how to avoid them
Teams often swap parts by appearance alone and miss critical geometry—this causes premature failure. Avoid mixing pins with different shoulder heights or groove placements. Don’t skip a trial run after installation; run the line at reduced speed for a full shift to check temperature and noise. Keep spare hinge pins and a basic repair kit close to the line to reduce mean time to repair.
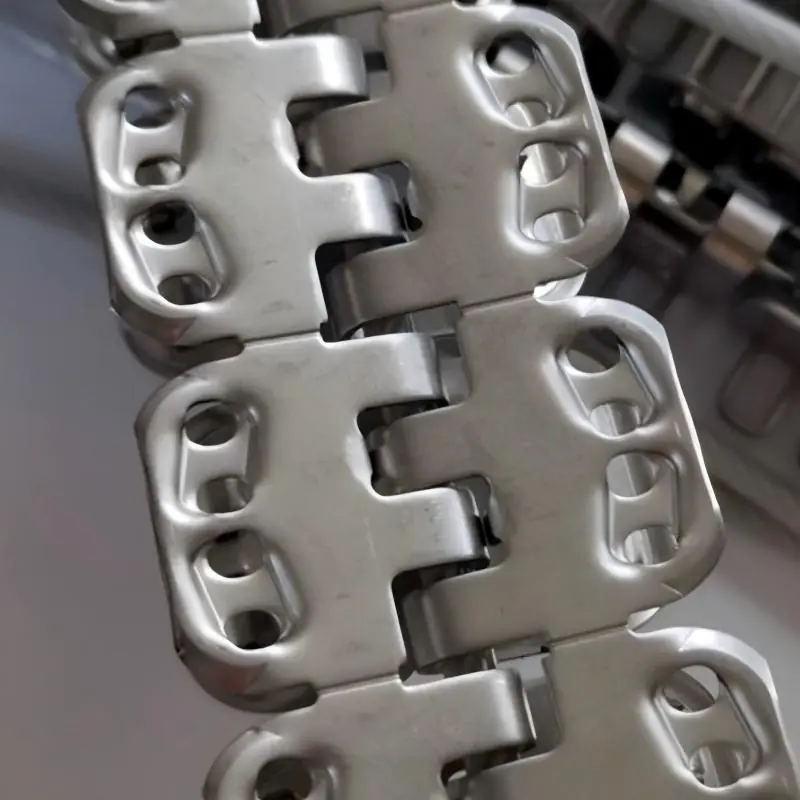
Real-world anchor and evidence
Field data from multiple midwestern assembly plants showed that replacing degraded hinge pins and correcting link plate alignment reduced unscheduled stops by roughly 22% over six months. Those findings guided the retrofit scope and helped justify spare-part inventory changes.
Maintenance rhythm and monitoring
Set a cadence: visual inspection weekly, measurement every month, and full joint rebuild quarterly for high-cycle sections. Track lubricant condition and ambient contamination. Use simple vibration checks and thermal scans to catch rising friction early—these diagnostics are practical and inexpensive. —A short weekly log makes long-term trends obvious and keeps teams accountable.
Advisory: three golden rules for selecting and fitting hinge pins
1) Match geometry precisely: diameter, shoulder, and groove placement must mirror originals or manufacturer drawings. 2) Prioritize material by environment: choose stainless hinge pins for corrosive or washdown areas; otherwise, hardened alloy is usually better for wear resistance. 3) Validate alignment under load: install, then test at operating speed for a full production cycle before declaring the job complete.
These rules reduce rework, improve uptime, and ensure parts purchased actually solve the problems maintenance faces. Final thought — attention to small details yields big reliability gains. Intake.